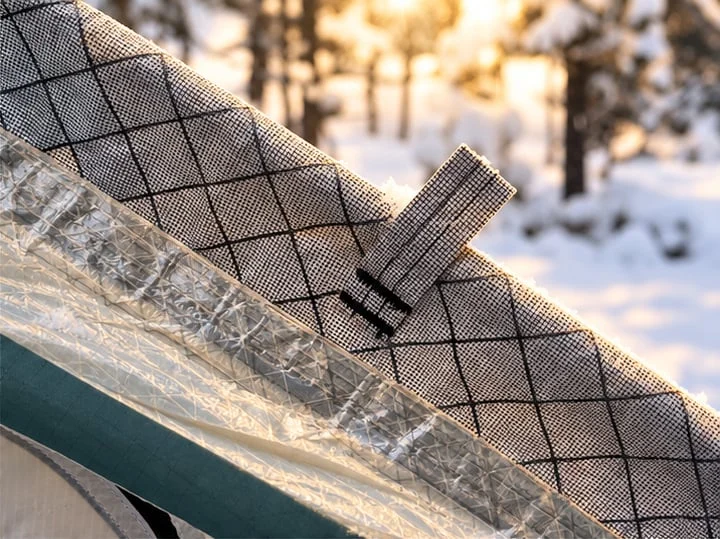
In the pursuit of the "ultralight" ideal, the modern backcountry traveler is faced with a dizzying array of material options. Technical fabrics—often categorized by broad families like DCF, Ultra, X-Pac, ECOPAK, silpoly, and silnylon—have revolutionized the weight-to-strength ratios of outdoor gear. However, simply identifying a fabric by its marketing name is no longer sufficient for serious design or purchasing decisions.
Individual constructions within these families differ substantially in mass, tear strength, abrasion resistance, waterproofness, dimensional stability, and construction methodology. Whether you are a custom gear maker (MYOG) or a consumer analyzing the specs of a high-end pack, understanding these nuances is essential to moving beyond "marketing hype" and into true engineering performance.
Main Facts: The Material Landscape
The fundamental challenge in technical fabric selection is that no single material performs optimally across all metrics. A fabric that excels in tear strength may be prohibitively stiff; a material with superior abrasion resistance may be too heavy for an ultralight shelter.
Technical fabrics are broadly split into three application categories: Packs, Shelters, and Storage Systems. Each demands a distinct set of mechanical and environmental compromises. For example, a pack must endure sustained structural loads and concentrated stress at stitching points, while a shelter must prioritize dimensional stability (resisting "wet sag") and wind-load management. Storage systems, conversely, require high flex durability to withstand the repetitive folding, rolling, and zipping inherent in daily use.
Chronology: The Evolution of Fabric Tech
The history of technical outdoor textiles is a move toward high-modulus, composite-based architectures.
- The Traditional Era: For decades, nylon and polyester wovens reigned supreme. Silnylon (silicone-impregnated nylon) became the industry standard for its flexibility and tear resistance. However, it suffers from significant "wet sag" as nylon fibers absorb moisture.
- The Composite Revolution: The introduction of Dyneema Composite Fabric (DCF) marked a paradigm shift. By sandwiching nonwoven Dyneema fibers between thin films, manufacturers achieved unparalleled weight-to-strength ratios and zero-stretch properties.
- The Modern Laminate Era: Today, we see the rise of "Woven Composites" like Challenge Outdoor’s UltraWeave. These materials address the primary weakness of early composites—low abrasion resistance—by using high-tenacity UHMWPE (Ultra-High-Molecular-Weight Polyethylene) woven face fabrics laminated to waterproof films.
- The Future—Fusion Bonding: The latest frontier, exemplified by ALUULA, involves thermoplastic composites that can be heat-welded. This moves the industry away from traditional needle-and-thread construction toward airtight, seamless, and potentially more durable structures.
Supporting Data: Understanding the Families
Dyneema Composite Fabric (DCF)
DCF utilizes nonwoven fibers in a 0/90-degree grid. It is the gold standard for weight reduction and waterproofness. However, the exposed film surface in standard DCF is prone to abrasion. "Hybrid" constructions (DCH) introduce a woven face fabric to solve this, albeit at a weight penalty.
Challenge UltraWeave
Designed for high-load applications, UltraWeave represents a significant departure from DCF. By using an Ultra-PE woven face, it carries structural loads while providing substantial surface durability. The "X" series (Ultra100X, 200X, 400X) scales these benefits based on denier and application.
X-Pac and ECOPAK
These represent the "sewn-laminate" architecture. They are reliable, predictable, and offer excellent stitch support. X-Pac, born from sailcloth technology, uses an "X-PLY" reinforcement grid to manage load, while ECOPAK focuses on using recycled materials and specialized backing structures to balance mass and durability.
Silpoly vs. Silnylon
The choice between these two remains a staple of shelter design. Silpoly (polyester) has largely overtaken silnylon for shelters because it is hydrophobic, meaning it doesn’t stretch when wet, allowing for a taut, stable pitch in rain or dew.
Technical Comparison Tables
Table 1: Backpack Fabrics
| Material | Weight (gsm) | Best Use | Primary Limitation |
|---|---|---|---|
| ROBIC 210D | 124.7 | General pack bodies | Lacks public technical data |
| X-Pac VX21 | 210 | Structured packs | Heavier than modern alternatives |
| Ultra200X | 155 | High-performance packs | Higher cost; film-backed complexity |
| DCH 3.2 | 104 | Light pack bodies | No standard abrasion rating |
(Note: Data is based on current manufacturer specifications. Always verify test methods before direct comparison.)
Table 2: Shelter Fabrics
| Material | Weight (gsm) | Wet Stability | Best Use |
|---|---|---|---|
| Silpoly 1.1oz | 42 | High | Conventional shelters |
| DCF 0.55 | 19 | Excellent | Min-mass shelters |
| UltraTNT | N/A | Excellent | Taped ultralight structures |
| ALUULA Aeris X | 32.9 | Excellent | Welded/Experimental |
Official Responses and Engineering Realities
The consensus among leading gear engineers is that "headline" specs—such as raw tear strength—are frequently misunderstood. A fabric with a massive tear strength rating can still fail if the stitch-holding capacity of the laminate is poor or if the material is too stiff to distribute stress at seam intersections.
Manufacturers like Challenge Outdoor and DSM (Dyneema) emphasize that durability is a localized phenomenon. Failure rarely occurs in the middle of a flat panel; it occurs at strap anchors, hipbelt interfaces, and compression zones. Therefore, the goal of a designer is not to find the "strongest" fabric, but the lightest fabric that maintains an adequate margin of safety at these specific high-stress points.
Implications: A Practical Selection Framework
When selecting materials, follow this hierarchical evaluation process:
- Define the Failure Mode: Is this product likely to fail via puncture (storage), abrasion (pack bottom), or tension-related stretch (shelter)?
- Evaluate Construction Compatibility: Can this material be effectively sewn? Does it require PSA (pressure-sensitive adhesive) tape or welding? Does the chosen construction method introduce new failure points?
- Analyze Localized Loads: For packs, ensure the fabric has enough "body" to support the reinforcement patches required at load-bearing anchors.
- Prioritize Flex Durability: For storage items, ignore high-modulus stats and focus on how the fabric handles being rolled and creased thousands of times.
- Environmental Reality: Consider the UV exposure and moisture cycling. If you are in a wet climate, avoid nylon-based materials that will sag, regardless of their other properties.
The Myth of "The Best"
The industry’s move toward specialized laminates proves that "the best" is a moving target. We are currently in a period of rapid innovation where we have the tools to engineer fabrics for specific micro-tasks. However, this complexity requires the user to be more educated than ever.
As we move toward a future of welded seams and fiber-fusion, the traditional rules of gear repair and construction are being rewritten. The most successful products of the coming decade will be those that balance these sophisticated new materials with an honest assessment of how they actually behave in the backcountry—not just how they look on a lab spreadsheet.
By looking beyond the marketing claims and evaluating fabric through the lens of application-specific engineering, users can ensure their gear is not just light, but reliable for the long haul. Whether you are traversing a mountain range or organizing a week’s worth of food, the right fabric choice turns a piece of equipment into a seamless extension of your adventure.